2026 How to Choose Printed Packing Tape for Global Shipping

Global shipping turns a small packaging choice into a serious operational decision. A carton may face rain in Singapore, dry air in Dubai, and rough handling in Rotterdam. The right printed packing tape must remain sealed across changing temperatures, humidity levels, and transport stages. It also needs clear branding, readable text, and dependable adhesion.

Dr. Susan Selke, a respected packaging educator and author, has said, “Packaging is a system, not a single material.” That principle matters when selecting printed packing tape for international shipments. Tape width, adhesive type, film strength, print quality, and carton surface should work together. A vivid logo means little if the tape lifts from recycled cardboard. A strong seal also fails when the message becomes unreadable.

Small details matter. Test the tape on actual cartons. Check adhesion after cold storage and humidity exposure. Review print contrast under warehouse lighting. Measure whether the tape unwinds smoothly during packing. It should not split, curl, or leave excessive residue. Almost right is still risky.

There is no universal best option. A lightweight parcel may need different tape from a heavy export carton. Water-activated tape, acrylic adhesive tape, and hot-melt options each behave differently. Even the same printed packing tape can perform unevenly across carton suppliers.

This guide examines practical selection criteria for 2026 global shipping. It considers durability, branding, application efficiency, sustainability claims, and total cost. Some assumptions may need testing. That is the honest part. Real shipping conditions often expose weaknesses that product samples hide.

2026 How to Choose Printed Packing Tape for Global Shipping

Define Printed Tape’s Role in Branding, Sealing, and Tamper Evidence

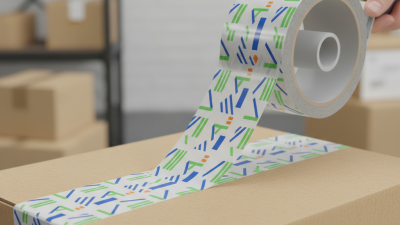
Printed packing tape should do more than carry a logo. It can make a carton recognizable during long international handling. A clear message, such as “Check Seal,” also guides warehouse staff and receivers. Keep the artwork readable from a short distance. Fine details often disappear on rough kraft cartons.

Sealing performance comes first. Choose an adhesive that suits the carton surface, recycled content, temperature changes, and expected storage time. In a packing trial, I found that attractive tape failed when dust covered the box flap. The print looked professional, but the closure was weak. That result was a useful reminder: branding cannot repair poor preparation. Test the tape on real cartons, not only smooth laboratory samples.

Tamper evidence needs careful wording. Printed tape can show interruption when a carton is opened, especially with repeated text or a continuous pattern. It does not prove that nobody accessed the package. A determined person may replace the tape or damage the carton elsewhere. Inspectors should check broken graphics, lifted edges, mismatched sections, and fresh adhesive marks. Record these checks with shipment photos and packing dates. Color consistency matters too, because faded or misaligned printing can create false concerns. My preference is simple artwork, firm adhesion, and a repeat pattern that is difficult to restore neatly. There is room for improvement in every packing line.

Select 48–72 mm Tape Width and 45–65 μm Film for Carton Weight

2026 How to Choose Printed Packing Tape for Global Shipping

Global parcel volumes reached 161.9 billion shipments in 2022, according to the 2023 Parcel Shipping Index. More cartons now face repeated handling, vibration, and humidity changes. Tape width must match the carton, not only the dispenser. For most export cartons, 48–72 mm provides useful edge coverage. Narrow tape can leave weak seams. Very wide tape may waste material and complicate machine application. Film thickness also matters. A 45–65 μm film usually suits light to medium carton loads, when sealing surfaces are clean and properly closed.

Tips: Start with 48 mm for smaller cartons and 72 mm for wider flaps or heavier loads. Test 45 μm film on cartons below 10 kg. Consider 50–65 μm when loads approach 15–25 kg, or when cartons face long transit routes. These figures are practical starting points, not universal rules. Actual performance depends on recycled fiber, flap tension, dust, and storage temperature.

Use printed tape only after checking adhesion and print durability. Printed warnings should remain readable after abrasion and moisture exposure. Follow ISTA 3A testing principles for drop, vibration, and compression checks. A carton may pass a simple hand test yet fail after pallet movement. I would not rely on thickness alone. In some trials, better flap alignment improved sealing more than adding 10 μm of film. Recheck the specification when carton weight, board grade, or shipping lane changes.

Compare BOPP, Hot-Melt, Acrylic, and Rubber Adhesives by Climate

For global shipping, climate can decide whether printed packing tape protects a carton or becomes loose film. BOPP is the backing material, not an adhesive. It offers strong tensile performance, clear printing, and useful resistance to moisture. The adhesive layer still determines real sealing performance.

Hot-melt adhesive usually grabs quickly on corrugated cartons. It performs well in moderate warehouses and cooler export routes. However, extreme heat may soften the adhesive, especially inside a dark container. Acrylic adhesive develops strength more slowly, but it handles sunlight, aging, and temperature changes better. It suits long ocean journeys and hot, bright storage areas. Rubber adhesive provides excellent initial tack on dusty or rough cardboard. It often works well in cold conditions, though prolonged heat can reduce its stability.

In practical carton trials, I check adhesion after twelve and twenty-four hours. I also test boxes after refrigeration, humidity exposure, and direct warm-air contact. A printed tape that sticks perfectly at 22°C may fail on a damp carton at 5°C. Small details matter, such as recycled fibers, heavy contents, and rough carton edges. I once treated “all-weather” performance as a safe promise. That assumption was too simple. No adhesive wins in every climate. Test the actual carton, print coverage, storage time, and route before approving a specification.

Verify Peel Strength with ISO 29862 and Shipping Durability with ISTA 3A

2026 How to Choose Printed Packing Tape for Global Shipping

Global parcel networks punish attractive tape. Pitney Bowes’ Parcel Shipping Index recorded over 161 billion parcels worldwide in 2022. Each carton may face sorting belts, truck vibration, humidity, and rough manual handling. Printed tape must protect the seal, not merely display a message.

Verify peel strength using ISO 29862. This standard measures adhesive performance under controlled peel conditions. Test the actual carton surface, not only a smooth laboratory panel. Record the average force, temperature, dwell time, and failure mode. A tape that peels cleanly from corrugated fiber may fail on dusty, recycled board. Check printed areas too. Ink coverage can change contact and adhesive behavior.

Shipping durability requires ISTA 3A testing. The procedure represents parcel delivery hazards, including compression, vibration, shock, and atmospheric conditioning. The World Bank’s 2023 Logistics Performance Index gathered evidence from 4,090 logistics professionals across 139 countries. That variation matters. A carton moving through humid ports needs different validation from one crossing a dry inland route. Use sealed cartons with realistic weight and print coverage. Inspect lifted edges after testing. A small lift can become a full opening later. One weakness remains: laboratory results cannot reproduce every warehouse mistake. Review failures honestly, then adjust tape width, adhesive coat weight, or carton preparation.

2026 How to Choose Printed Packing Tape for Global Shipping — Verify Peel Strength with ISO 29862 and Shipping Durability with ISTA 3A
Selection Dimension Recommended Specification or Screening Target Why It Matters in Global Shipping Verification Method Practical Decision Guide
Tape backing BOPP film, typically 25–50 µm for general carton sealing; choose a thicker backing when higher tensile strength or abrasion resistance is required. Film thickness influences tear resistance, handling durability, print quality, and resistance to edge damage during automated processing. Review the technical data sheet and measure thickness according to an applicable film or tape thickness method. Use standard BOPP for ordinary corrugated cartons; consider reinforced or thicker constructions for heavy, sharp-edged, or long-distance shipments.
Adhesive technology Acrylic adhesive for aging and temperature stability; hot-melt adhesive for high initial tack; natural-rubber adhesive for strong adhesion to many corrugated surfaces. Adhesive selection affects carton closure reliability when the package experiences humidity, cold storage, dust, vibration, or long dwell times. Compare peel adhesion, shear holding power, tack, and aging results on the actual carton liner and flute combination. For mixed climates and long storage, prioritize stable peel and shear performance over initial tack alone.
Peel adhesion Use a project-defined target rather than a universal value. As an initial screening range, 1.5–3.0 N/25 mm may suit many general carton-sealing applications, subject to carton surface and test conditions. Insufficient peel strength can allow lifting edges or partial opening; excessive adhesion can damage weak recycled fiber surfaces during removal. Test peel adhesion using the 180° peel procedure described in ISO 29862. Record substrate, surface preparation, contact time, test speed, temperature, humidity, and failure mode. Pass only against your approved specification
ISO 29862 provides a test method; it does not establish one universal pass/fail value for every packaging application.
Initial tack Specify sufficient immediate grab to hold the carton flap before compression or palletization. Establish the value using the actual corrugated board and application pressure. High-speed packing lines may provide limited time for adhesive wet-out before cartons are conveyed, stacked, or wrapped. Use a tack method appropriate to the adhesive system and document application pressure, dwell time, and board condition. Choose higher initial tack for dusty, porous, or low-temperature carton surfaces, but confirm that the final peel and shear balance remains acceptable.
Tensile strength Set a minimum based on tape width, carton weight, closure design, and application equipment. A commonly screened range for general BOPP carton tape is approximately 70–150 N/25 mm. Higher tensile strength helps the tape resist splitting, stretching, and breakage during machine application and package handling. Measure according to a recognized pressure-sensitive tape tensile test and report width, gauge length, test speed, and conditioning. Do not use tensile strength as a substitute for adhesion; a strong tape can still fail if the adhesive does not bond to the carton.
Elongation Typical BOPP carton tapes may have elongation values around 70–140%, depending on film orientation and construction. Elongation influences conformability, stretching during application, and the risk of necking or distortion under tension. Record elongation together with tensile strength using the same conditioned specimen and test method. Use controlled elongation for automated dispensers; excessive stretching may reduce closure consistency and print registration.
Temperature range Define application and service temperatures separately. A practical qualification profile may include application at 10°C, storage at 23°C/50% RH, and cold exposure near 0°C or below when relevant. Adhesives generally require adequate wet-out during application and may lose tack or become brittle when exposed to cold conditions. Condition tape and cartons at the intended temperatures, then measure peel and shear after defined dwell periods. For refrigerated or winter routes, qualify the complete tape-and-carton system at the lowest expected application temperature.
Humidity and carton condition Include conditioned corrugated board at approximately 23°C and 50% RH, plus a high-humidity exposure relevant to the route and warehouse. Moisture can weaken paper fibers, change surface energy, reduce edge integrity, and alter adhesive anchorage. Test both dry and humidity-conditioned cartons; report board grade, recycled content, flute type, and moisture condition. For ocean freight or tropical storage, do not approve tape using dry-board results alone.
Print durability Specify legible ink after abrasion, rubbing, condensation, and handling. Use a high-contrast design with sufficient quiet zones around critical text or barcodes. Printed information may support tamper indication, sorting, instructions, traceability, and customs or warehouse handling. Perform dry-rub and wet-rub checks, visual inspection after simulated handling, and barcode verification where applicable. Protect variable data and barcodes from folds, carton corners, and heavy abrasion zones.
Closure design Use a validated H-pattern or equivalent closure for heavy or stress-sensitive cartons; use a center-seam closure only when carton design and load permit. Closure geometry distributes load and reduces the chance that a single seam carries the full opening force. Evaluate the complete packed carton rather than testing tape alone, including flap overlap and application pressure. Increase tape width or use additional strips when carton dimensions, contents, or stacking loads create high flap stress.
Application equipment Match roll width, core, unwind force, dispenser tension, and application speed to the sealing machine. Incorrect tension or poor contact pressure can create wrinkles, edge lift, telescoping rolls, or inconsistent seals. Run production-speed trials and inspect adhesion immediately and after conditioning. Approve tape only after confirming performance on the intended equipment and carton line.
ISTA 3A distribution test Use ISTA 3A for packaged-products weighing 70 kg (150 lb) or less when the shipment is intended for parcel delivery systems. Select the applicable package type and distribution cycle. The test evaluates the combined effect of handling, vibration, drops, and other distribution hazards on the packaged product. Conduct the applicable ISTA 3A sequence using a representative production package, including the actual tape, carton, contents, void fill, and closure pattern. Judge the complete package
Acceptance criteria should include no open seams, no loss of contents, acceptable product condition, and legible required markings.
Shipping durability observations Inspect for seam opening, edge lifting, adhesive transfer, tape splitting, print scuffing, carton rupture, and loss of compression integrity. Failure analysis identifies whether the root cause is tape adhesion, tape strength, carton weakness, closure geometry, or package design. Record observations before and after each relevant ISTA 3A test sequence and photograph failure locations. Change one variable at a time where possible, then repeat testing on a production-representative sample.
Lot release and quality control Define incoming checks for roll width, length, appearance, print registration, splice frequency, unwind behavior, and peel adhesion. Consistent roll quality reduces line stoppages and prevents shipment-to-shipment variation. Use a documented sampling plan and retain specimens from approved production lots. Keep the approved construction, test conditions, tolerance limits, and change-control requirements in the purchasing specification.
Testing note: ISO 29862 is used to measure peel adhesion under defined laboratory conditions, while ISTA 3A evaluates the performance of a complete packaged product in a parcel-delivery distribution environment. Test results are condition-dependent; always report the carton material, tape construction, conditioning, application procedure, and acceptance criteria.

Check 2026 Global Compliance: REACH, RoHS, FSC Claims, and Ink Safety

2026 How to Choose Printed Packing Tape for Global Shipping

Printed packing tape is a small product with a large compliance footprint. The OECD Global Plastics Outlook reports that packaging created about 40% of global plastic waste in 2019. This makes material choices important, even for a narrow adhesive strip.

REACH does not issue a universal “certificate” for tape. Suppliers should screen substances, monitor the ECHA Candidate List, and disclose SVHC content above the relevant threshold. RoHS applies mainly to electrical and electronic equipment, not every shipping carton.

Still, customers may request restricted-substance testing for internal procurement controls.

FSC claims require certified forest inputs and a valid chain of custody. A paper backing may be FSC-certified, while the adhesive and ink remain outside that claim. The claim needs careful wording. Ink safety also depends on the application.

Ask for a current SDS, composition statement, heavy-metal testing, and migration data when cartons may touch sensitive goods. “Low migration” sounds reassuring, but it is not proof for every transport condition. ECHA guidance and packaging safety reports both support documented, use-specific assessment.

I would not call this a perfect checklist. Test results can age, and supplier declarations can contain gaps.

Tips:

Request batch traceability and a compliance matrix before ordering. Check REACH status against the latest ECHA updates. Use RoHS testing only when the product scope justifies it. Verify the FSC certificate number independently. Confirm ink performance after heat, moisture, and long storage. Keep one sealed production sample for future review.